 English
 English
 русский
 日本語
 Español
 中文简体
The SANTO UFA range of self-regulating heating cables is mainly used for frost protection of pipes and vessels but can also be used to maintain processes up to 65°C. These heating cables are available...
See Details
Content
Industrial heating systems must perform reliably in environments where ordinary electrical cables, household heating products, and low-temperature tracing solutions can quickly deteriorate. High temperatures, corrosive chemicals, moisture, mechanical impact, explosive atmospheres, and long operating cycles all place demanding requirements on the heating cable. The XPI Polymer Insulated (PI) Series Resistive Heating Cable is designed for these conditions. It combines a high-temperature nickel-plated conductor, multilayer fluoropolymer insulation, a nickel-plated copper protective braid, and a final PTFE jacket to create a durable solution for industrial heat tracing and constant-power heating.
The cable belongs to the series constant-power heating cable category. Its resistance is selected according to the required heating output, installation length, operating voltage, and process temperature. This enables designers to choose from a wide range of resistance models, from low-resistance versions for higher current applications to high-resistance versions for longer circuits or specific power requirements.
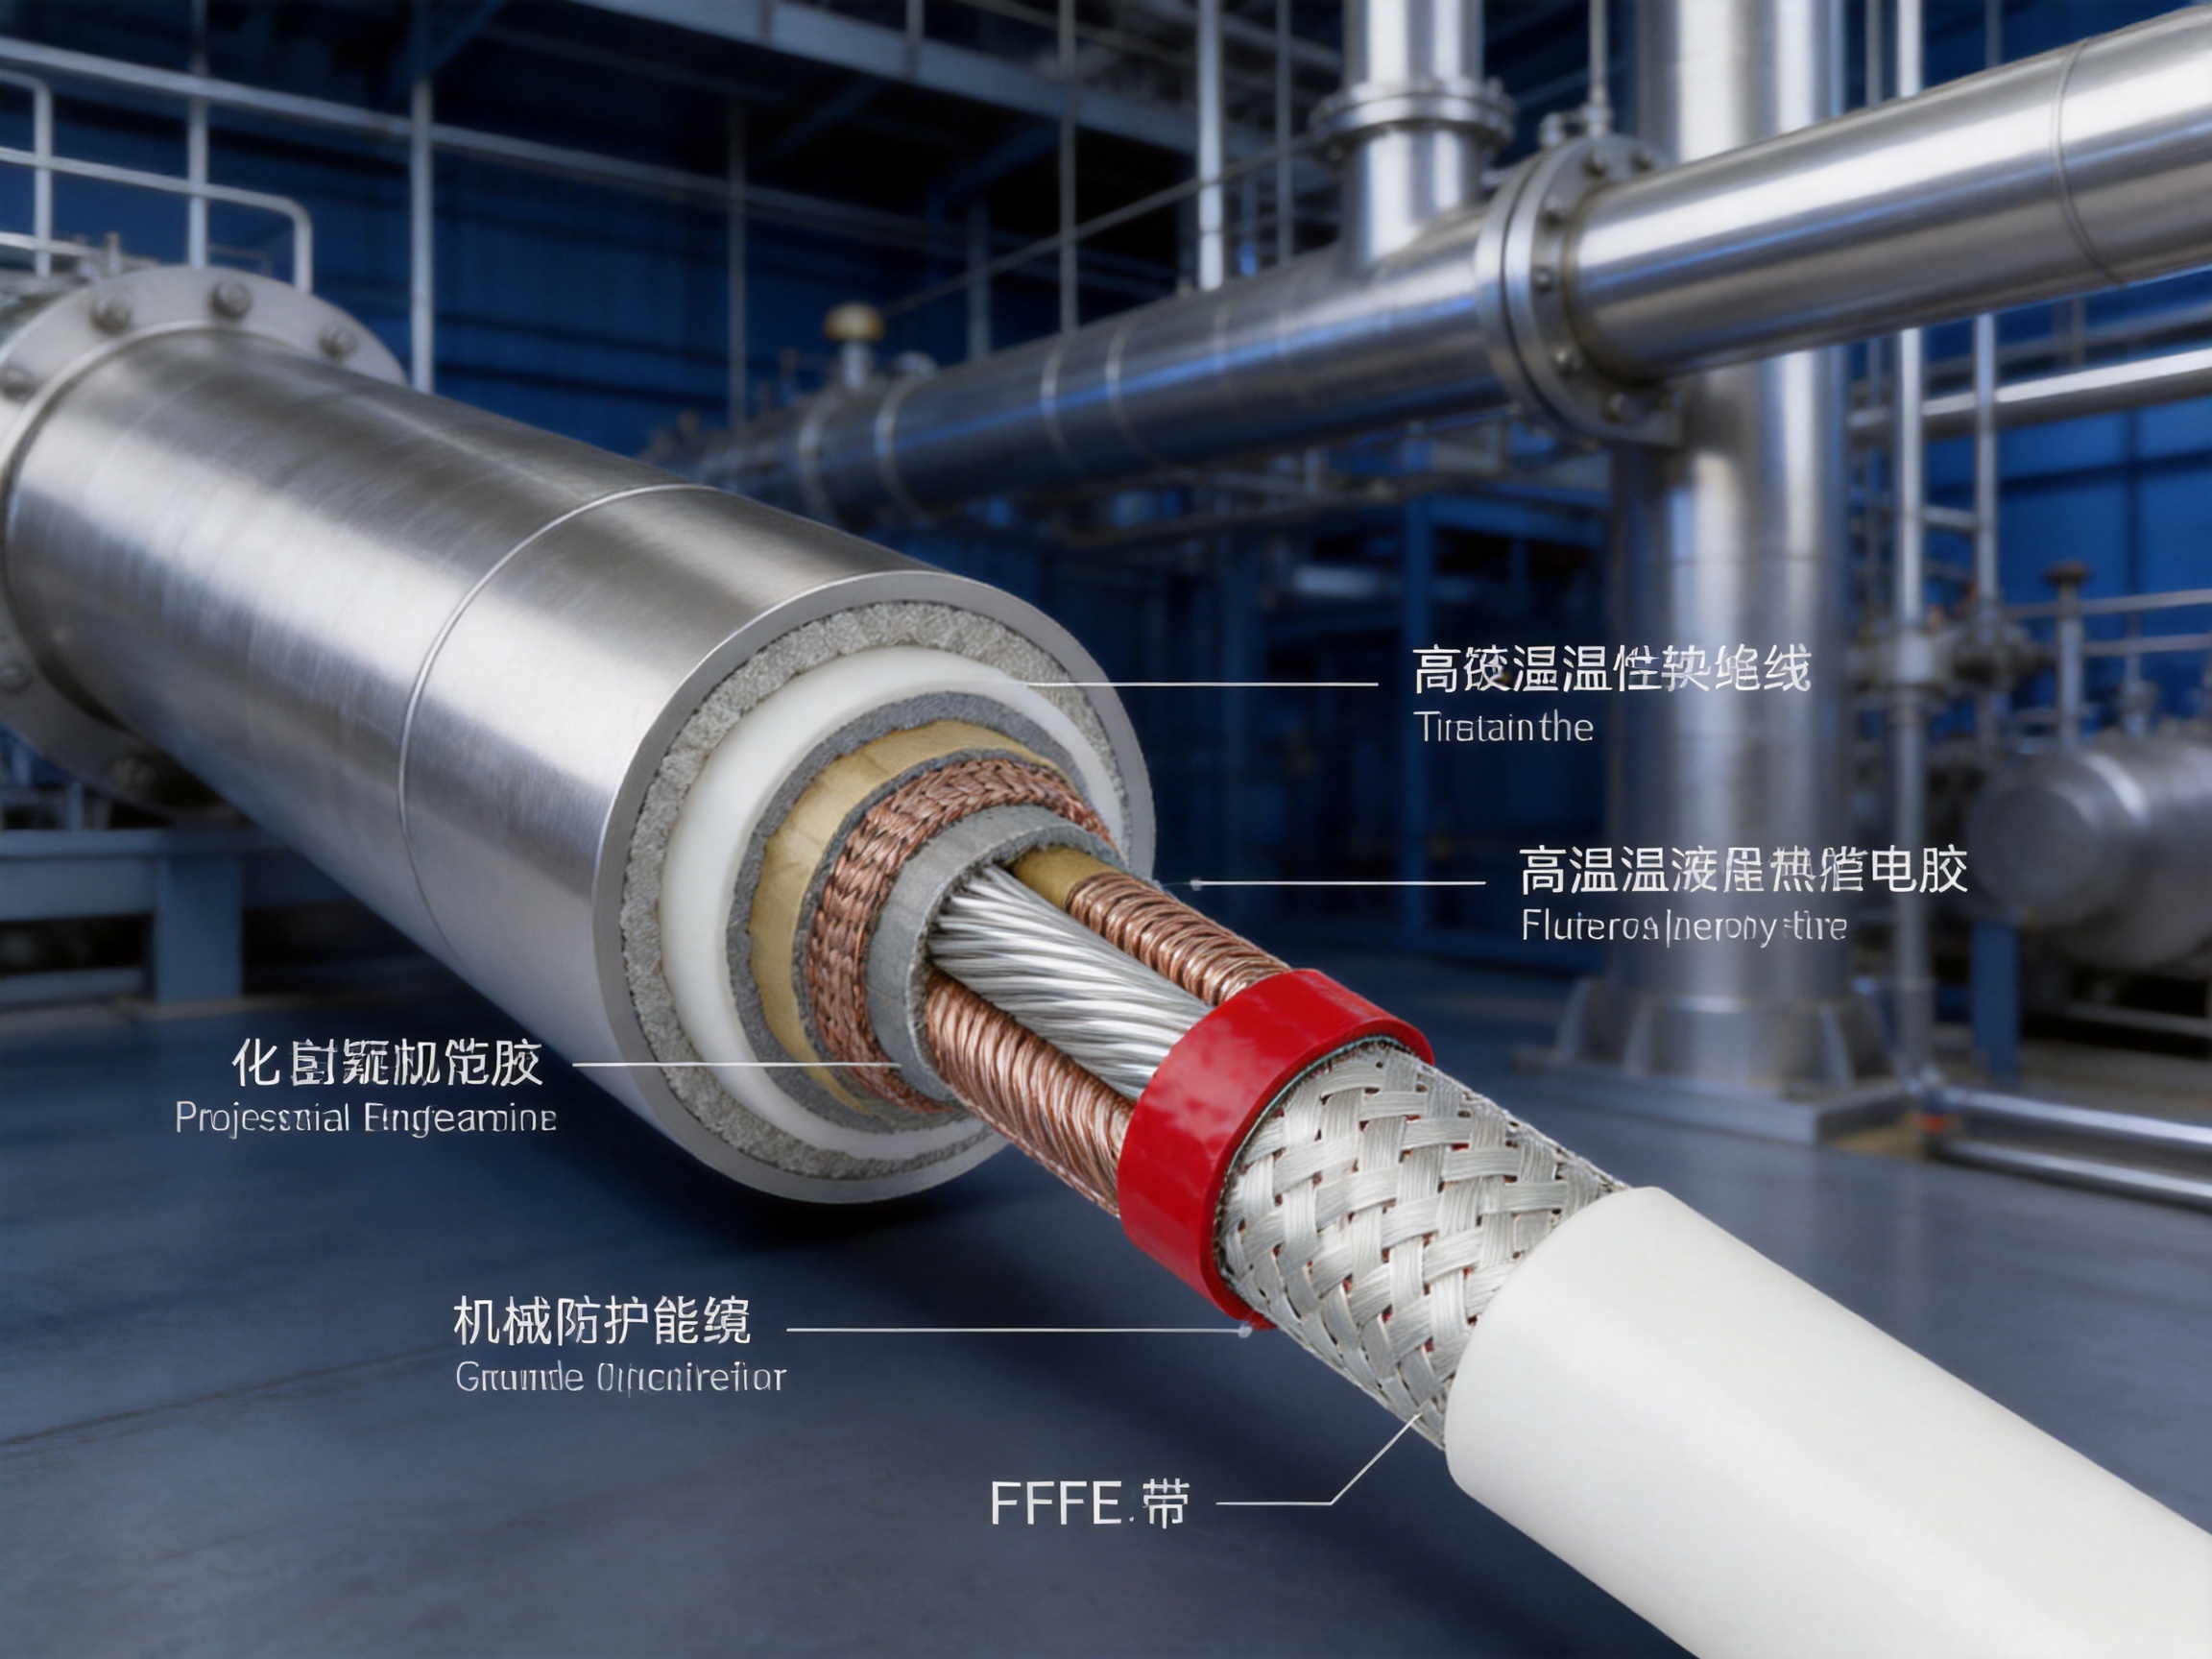
Unlike basic heating wires that depend on a single insulation layer or are limited to relatively mild environments, the XPI design uses a carefully arranged sandwich construction. Each layer performs a specific function. The nickel-plated stranded conductor supports long-term electrical performance at elevated temperatures and in corrosive surroundings. High-temperature fluoropolymers provide electrical isolation. The metal braid adds mechanical protection and provides a low-resistance earth path. The PTFE outer jacket improves resistance to chemicals, moisture, and high operating temperatures.
This construction makes the cable suitable for pipeline heat tracing, process equipment heating, tank and vessel heating, freeze protection, temperature maintenance, chemical service, and other industrial applications. It can also be considered for hazardous-area installations when the complete heating system is designed, installed, controlled, and certified in accordance with the applicable requirements.
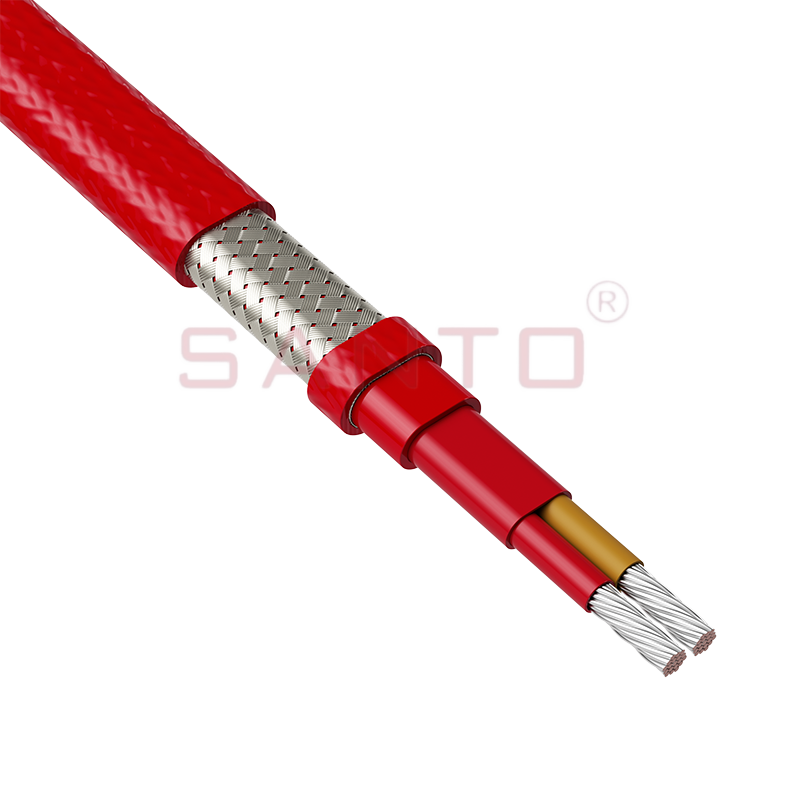
XPI Polymer Insulated (PI) Series Resistive Heating Cable
The XPI Polymer Insulated Series is a resistive heating cable engineered for industrial heat tracing systems. The heating effect is generated when electrical current passes through the conductor. The selected resistance determines the relationship between voltage, current, cable length, and heat output. Because the cable is available in many resistance values, the system can be adapted to different line lengths and heating duties.
The product range includes models from XPI-0.8 to XPI-8000. The number in the model designation generally corresponds to the standard resistance in ohms per kilometer at 20°C. The available range allows a project engineer to select a cable that matches the desired current, circuit length, voltage, and installed power.
Representative models include XPI-0.8, XPI-1.1, XPI-1.8, XPI-2.9, XPI-4.4, XPI-7, XPI-10, XPI-15, XPI-17.8, XPI-25, XPI-31.5, XPI-50, XPI-65, XPI-80, XPI-100, XPI-150, XPI-180, XPI-200, XPI-320, XPI-380, XPI-480, XPI-600, XPI-700, XPI-810, XPI-1000, XPI-1440, XPI-1750, XPI-2000, XPI-3000, XPI-4000, XPI-4400, XPI-5160, XPI-5600, XPI-7000, and XPI-8000.
The nominal outside diameter varies by model and is approximately 4.1 to 11.9 millimeters. Standard cable weight varies according to the conductor and construction, with listed values ranging from approximately 40 to 404 kilograms per kilometer. These dimensions make it possible to select a comparatively compact cable for many industrial installations while retaining the mechanical strength required for field use.
The stranded conductor is nickel-plated. Nickel plating is important in applications where the heating conductor is repeatedly exposed to elevated temperature or to an atmosphere that could accelerate oxidation or corrosion. The stranded structure also contributes to flexibility compared with a single solid conductor of equivalent cross-sectional area.
The conductor is surrounded by selected high-temperature fluoropolymers in a multilayer sandwich arrangement. This insulation system separates the electrical conductor from the protective braid and the surrounding equipment. Fluoropolymers are selected for their combination of temperature stability, chemical resistance, low moisture absorption, and electrical insulation performance.
A braid made from nickel-plated copper strands surrounds the insulation. This braid serves two important purposes. First, it improves resistance to abrasion, impact, and installation-related mechanical stress. Second, it provides a low-ohmic protective earth path. The earth braid can help support the protective strategy of the overall heating circuit when correctly terminated and connected to the grounding system.
The final PTFE jacket forms the external barrier. PTFE is widely valued for chemical resistance and high-temperature capability. In an industrial heat tracing system, this external layer helps protect the underlying electrical construction from process chemicals, oils, solvents, moisture, and other environmental influences. The jacket also makes the cable easier to clean and maintain in many industrial settings.
| Parameter | Specified value |
|---|---|
| Product type | Polymer-insulated series resistive heating cable |
| Heating category | Series constant-power heating cable |
| Maximum continuous exposure temperature | 260°C |
| Maximum intermittent exposure temperature | 300°C, up to 1,000 hours |
| Minimum installation temperature | -70°C |
| Maximum power output | 30 W/m standard value, depending on application |
| Rated voltage | Up to 450/750 VAC, U0/U |
| Minimum impact resistance | 4 joules according to the supplied EN 50019 reference |
| Minimum spacing between heating lines | 20 mm |
| Resistance reference temperature | 20°C |
| Standard resistance tolerance | +10% / -5%, according to the supplied product information |
The stated continuous exposure temperature is 260°C, while the intermittent exposure temperature is 300°C for up to 1,000 hours. These values describe the cable’s exposure capability and should not automatically be interpreted as the permitted process temperature in every installation. The allowable temperature depends on the complete system, including the heating cable, termination kits, control equipment, insulation, mounting method, process surface, hazardous-area classification, and applicable standards.
The minimum installation temperature is listed as -70°C. This is especially valuable for projects located in cold climates, refrigerated process areas, outdoor facilities, and winter construction environments. Installation teams should still follow project-specific handling instructions because bending flexibility, jacket behavior, and termination procedures can be affected by extremely low temperatures.
The standard maximum power output is listed as 30 watts per meter, with the specific value depending on the application. Heat output should be selected according to heat loss calculations rather than simply using the maximum value. Excessive power density can create undesirable surface temperatures, while insufficient power can result in poor temperature maintenance or freezing.
The rated voltage is up to 450/750 VAC, expressed as U0/U. The actual operating voltage must be selected according to the cable model, circuit length, supply arrangement, insulation system, protection equipment, and local electrical requirements. Correct voltage selection is essential because the heating power is directly affected by voltage and resistance.
The minimum listed impact resistance is 4 joules. The protective braid and PTFE jacket work together to provide a stronger external construction than an unjacketed resistive wire. Nevertheless, the cable should not be treated as indestructible. Routing should avoid sharp edges, repeated crushing, unauthorized drilling, and direct exposure to mechanical loads for which the system was not designed.
Resistance selection is one of the most important steps in designing a series heating cable system. For a resistive load, the basic relationships are expressed by Ohm’s law and the power equation. Current can be estimated using I = V/R, while total electrical power can be estimated using P = V²/R. For a cable with a known resistance per unit length, the total resistance depends on the installed length and the selected model.
These equations are useful for preliminary design, but they must be applied with consideration for conductor temperature. The supplied information notes that the resistance of conductive materials is a function of temperature and must be taken into account during design. The listed temperature coefficient provides an indication of how resistance changes with temperature. A cable that is rated at a particular resistance at 20°C may have a different resistance during operation.
For lower-resistance models, current is generally higher for a given voltage and circuit length. These models can be suitable when higher current capacity is acceptable and when the circuit length is relatively short or the power requirement is substantial. Higher-resistance models draw less current at the same voltage and may be useful for longer circuits, lower-power heating duties, or circuit designs that benefit from reduced current.
Designers should consider voltage drop, circuit length, startup behavior, ambient temperature, process temperature, thermal insulation, heat loss, and control strategy. The cable should be selected so that the heating output is adequate under the coldest expected conditions while avoiding excessive temperature during low-load or abnormal operating conditions.
For systems installed in hazardous locations, the electrical design must also consider maximum surface temperature, ignition protection, earth continuity, leakage current, equipment grouping, temperature classification, and the requirements of the relevant certification system. The supplied application information identifies gas Zones 1 and 2 and dust Zones 21 and 22 as applicable regional levels. Final suitability must be confirmed for the complete certified assembly, not only the cable itself.
| Model | Standard resistance at 20°C | Approximate outside diameter | Standard weight |
|---|---|---|---|
| XPI-0.8 | 0.8 ohm/km | 11.9 mm | 404 kg/km |
| XPI-2.9 | 2.9 ohm/km | 6.9 mm | 143 kg/km |
| XPI-7 | 7.0 ohm/km | 5.5 mm | 83 kg/km |
| XPI-25 | 25.0 ohm/km | 4.9 mm | 57 kg/km |
| XPI-100 | 100 ohm/km | 5.2 mm | 67 kg/km |
| XPI-480 | 480 ohm/km | 4.7 mm | 51 kg/km |
| XPI-1000 | 1,000 ohm/km | 4.5 mm | 48 kg/km |
| XPI-4000 | 4,000 ohm/km | 4.2 mm | 42 kg/km |
| XPI-8000 | 8,000 ohm/km | 4.1 mm | 40 kg/km |
The table illustrates the broad selection available. Low-resistance models use larger conductors and have greater weight per kilometer, while many high-resistance models have smaller outside diameters and lower standard weights. The correct model should be determined by a formal design calculation and confirmed against the manufacturer’s current technical documentation.
The XPI series offers several advantages over simpler heating wires and general-purpose cables. The first is temperature capability. Many standard polymer-insulated cables are intended for ordinary ambient or moderate process conditions. The XPI construction is designed for continuous exposure up to 260°C and intermittent exposure up to 300°C under the stated conditions.
The second advantage is chemical resistance. Industrial heat tracing often takes place near acids, alkalis, hydrocarbons, solvents, cleaning agents, salt solutions, and corrosive vapors. A final PTFE jacket and fluoropolymer insulation can provide a stronger barrier against many organic and corrosive substances than conventional PVC or lower-temperature elastomeric materials.
The third advantage is the combination of electrical insulation and mechanical protection. A single insulation layer may protect against electrical contact but offer limited resistance to abrasion or impact. The nickel-plated copper braid adds a separate mechanical layer and creates an earth path. This layered approach can improve durability during installation and operation.
The fourth advantage is design flexibility. The wide resistance range supports different circuit lengths and power requirements. Instead of forcing every project to use the same resistance and circuit arrangement, the engineer can choose a model that better suits the actual electrical and thermal conditions.
The fifth advantage is suitability for demanding outdoor and industrial environments. The minimum installation temperature of -70°C supports cold-weather projects, and the construction is intended for applications where moisture, chemicals, temperature cycling, and mechanical handling are present.
Compared with self-regulating heating cables, a series resistive cable does not automatically reduce its output in exactly the same way as a self-regulating product when the surrounding temperature changes. This means it requires more deliberate system design and temperature control. However, it can offer advantages where long circuits, high temperatures, controlled constant power, or specific resistance values are required. The best solution depends on the application rather than on a universal preference for one cable technology.
Compared with mineral-insulated cables, polymer-insulated construction may be easier to handle and terminate in some project conditions. Mineral-insulated products can offer exceptional temperature performance, but they may require specialized handling, bending procedures, and termination methods. The XPI series provides a balance between high-temperature operation, chemical resistance, mechanical protection, and installation practicality.
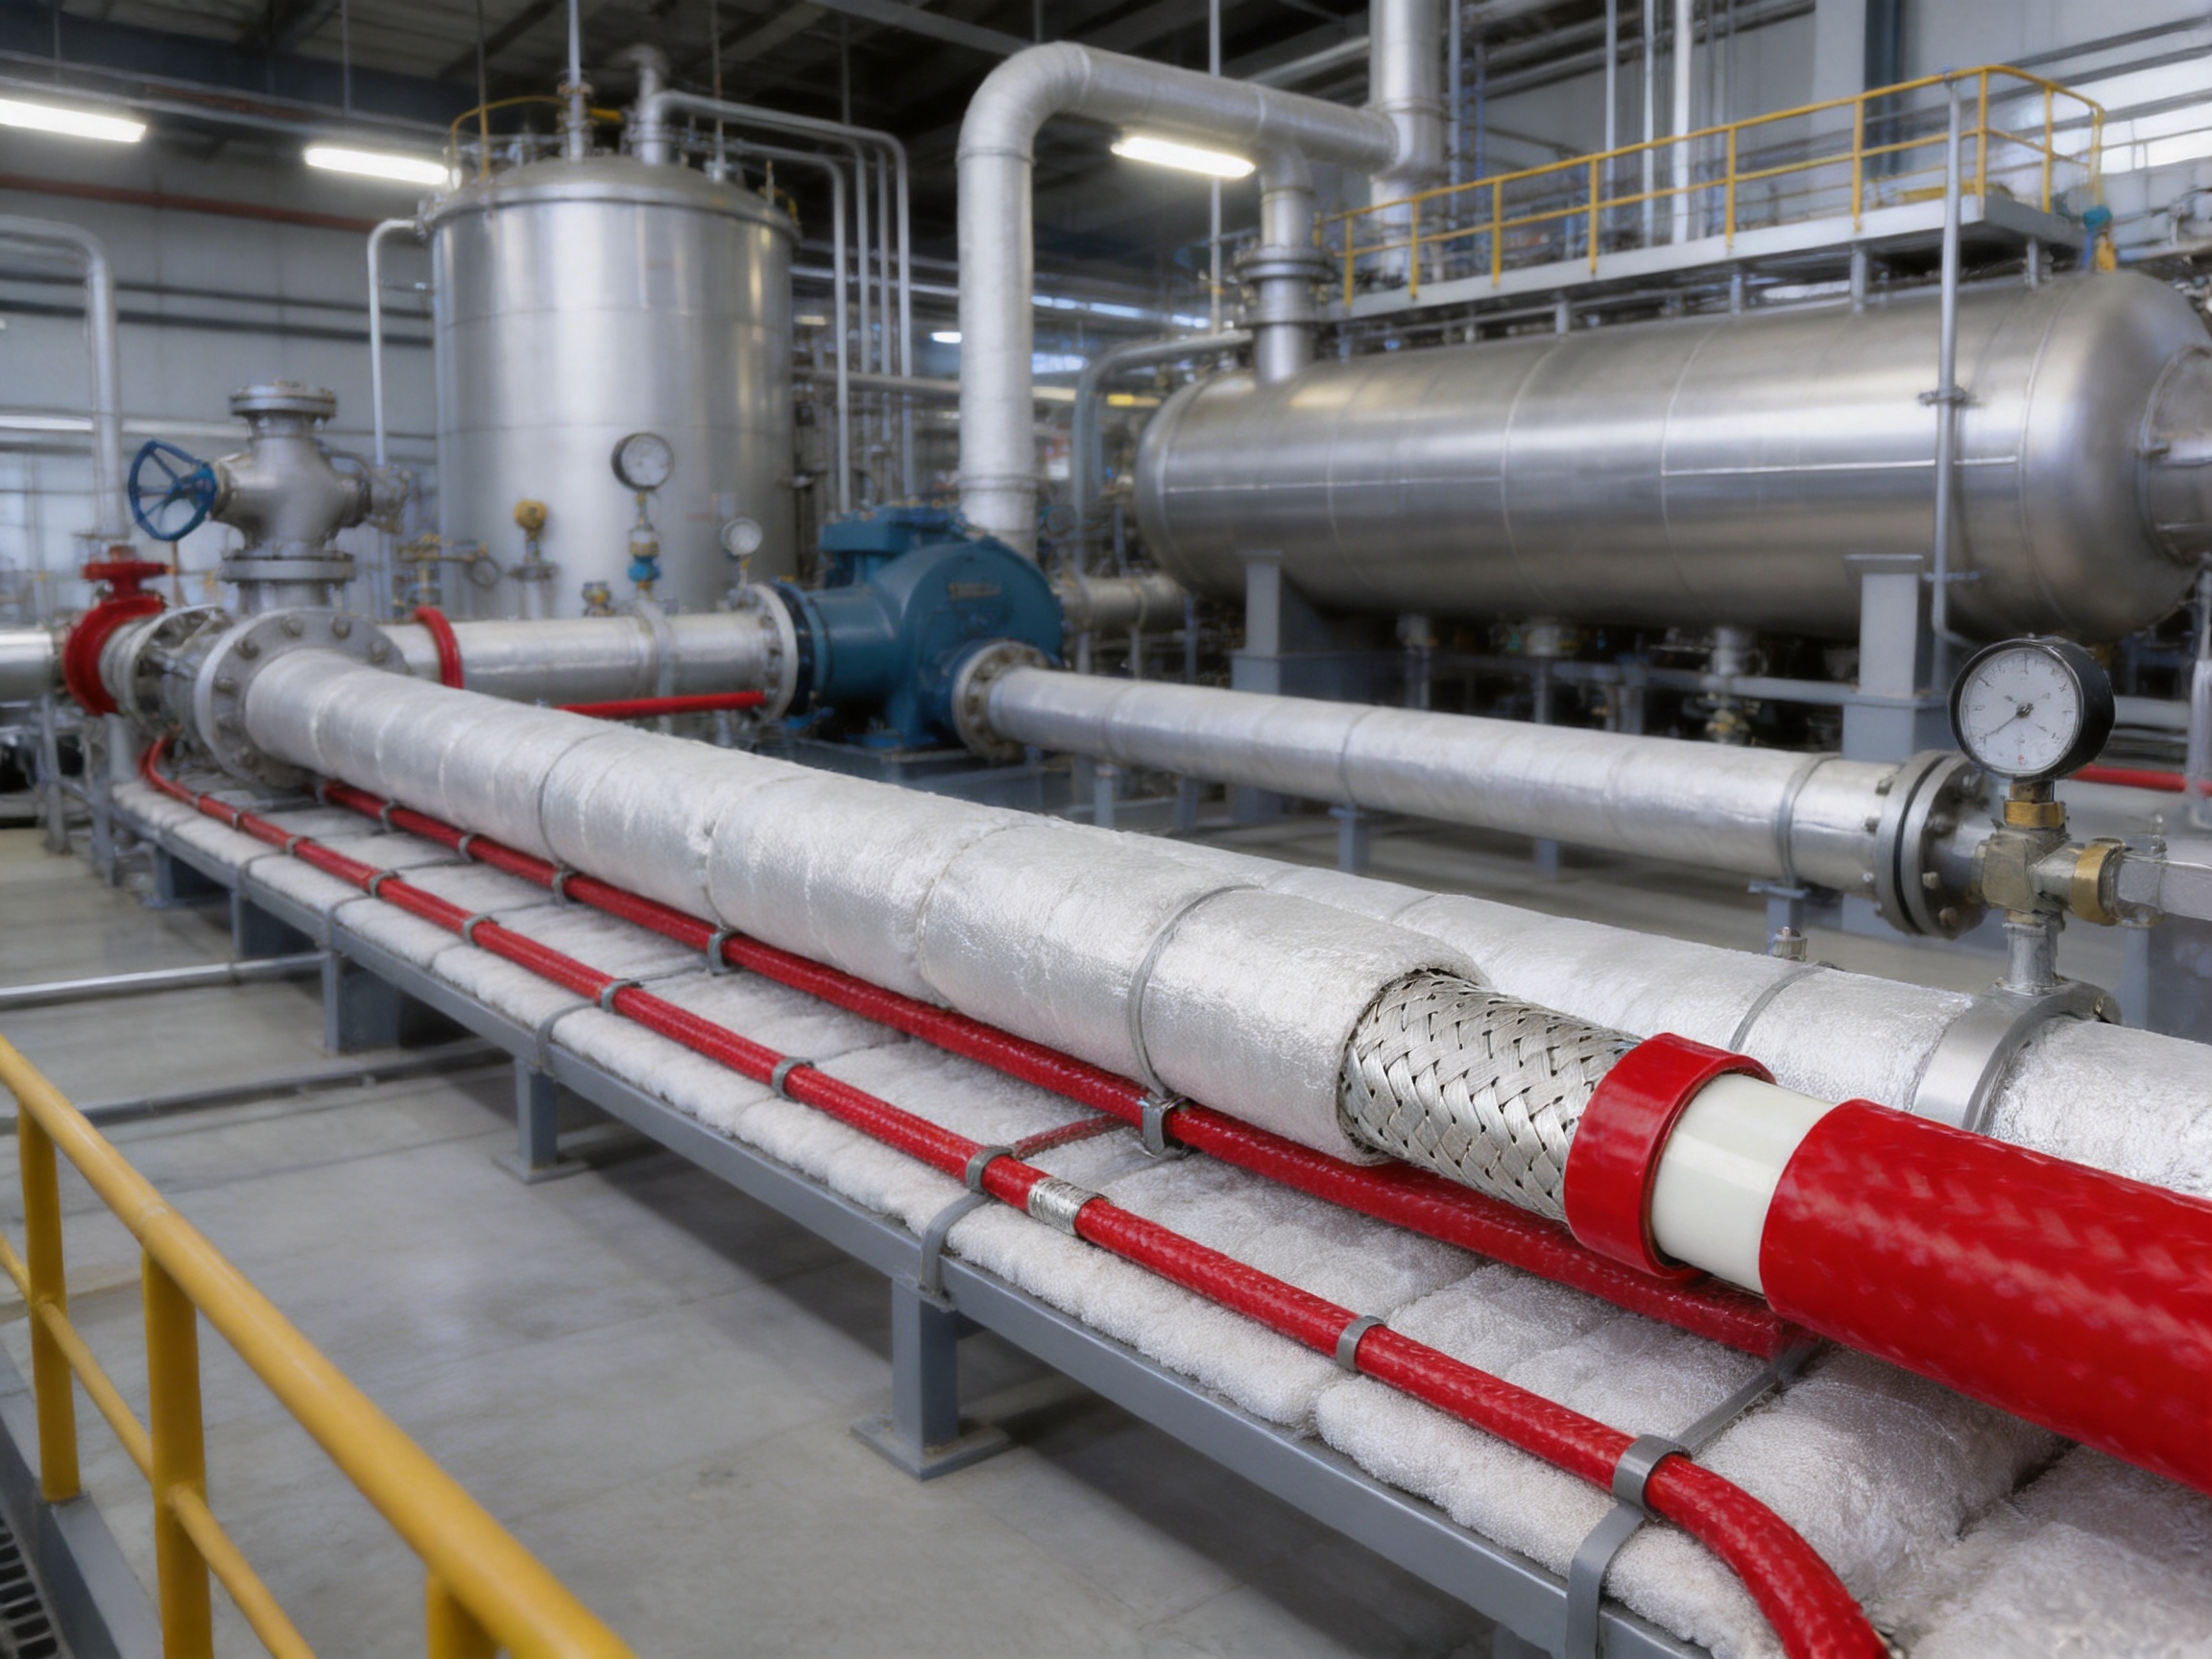
Pipeline heat tracing is one of the most important applications for industrial heating cable. A pipeline may require heating to prevent freezing, maintain viscosity, compensate for heat loss, or keep a process fluid within a specified operating range. The XPI series can be selected for pipelines carrying chemical products, oils, process liquids, gases, and other materials that must remain within a controlled temperature range.
The cable may be installed longitudinally along the pipe, spirally around the pipe, or according to a project-specific layout. Aluminum tape, stainless-steel bands, or other approved fixing methods may be used to improve heat transfer and hold the cable in position. The selected method must avoid crushing or damaging the PTFE jacket and must maintain the specified spacing between adjacent heating lines.
Valves, flanges, strainers, pumps, supports, and instrument connections often lose more heat than the straight pipe. They can also create locations where liquid collects and freezes. A flexible heating cable can be routed around these components when the bending radius, temperature limit, spacing, and installation instructions are observed.
Designers should account for the additional surface area and heat loss of fittings. A heating layout that is adequate for a straight pipe may not be sufficient for a valve or pump body. The cable should be distributed evenly, and local hot spots should be avoided.
Storage tanks and process vessels may need heating to maintain product flow, avoid crystallization, support chemical reactions, or prevent freezing. The XPI series can be arranged on tank walls, conical sections, vessel bottoms, or selected heat-loss zones. The design must consider the vessel material, insulation system, maximum wall temperature, liquid level, empty-vessel conditions, and the possibility of heat accumulation.
When a vessel can operate empty, temperature control becomes especially important. A cable designed for a fully loaded vessel may create a higher surface temperature when the liquid no longer absorbs heat. Independent temperature limiters, sensors, and suitable control logic should therefore be considered.
Industrial equipment such as filters, separators, hoppers, loading arms, transfer lines, and chemical dosing systems may require localized heat tracing. The chemical resistance of the outer jacket is useful where the cable may be exposed to process residues or cleaning chemicals.
Outdoor piping, fire-protection lines, drainage systems, water lines, and process utilities may require freeze protection during low ambient temperatures. The required power is usually determined by the pipe diameter, insulation thickness, wind exposure, ambient design temperature, and desired maintenance temperature. The XPI cable can be selected for these conditions, provided that the circuit and temperature control are correctly designed.
The supplied product information references gas Zones 1 and 2 and dust Zones 21 and 22. Such environments require careful control of ignition risks. The cable, cold lead, connection accessories, control equipment, glands, junction boxes, sensors, and installation method must all be appropriate for the classified area.
A heating cable should never be selected for a hazardous location solely because its insulation can withstand a certain temperature. The complete installation must satisfy the relevant explosion-protection requirements. Surface temperature must remain below the applicable temperature class or ignition temperature limit, and all electrical protection measures must be verified.
The recommended cold-end wire options are matched to several XPI models. The cold-end wire provides the connection between the heating section and the power supply or control equipment. Matching the cold-end conductor to the heating cable is essential because the cold end must carry the required current while maintaining insulation integrity and mechanical reliability.
| Cross-section | Current rating | Outside diameter | Resistance at 20°C | Matched model |
|---|---|---|---|---|
| 2.5 mm² | 32 A | 5.5 mm | 7.0 ohm/km | XPI-7 |
| 4 mm² | 42 A | 6.1 mm | 4.4 ohm/km | XPI-4.4 |
| 6 mm² | 54 A | 6.9 mm | 2.9 ohm/km | XPI-2.9 |
| 10 mm² | 73 A | 8.6 mm | 1.8 ohm/km | XPI-1.8 |
| 16 mm² | 98 A | 10.1 mm | 1.1 ohm/km | XPI-1.1 |
| 25 mm² | 129 A | 11.9 mm | 0.8 ohm/km | XPI-0.8 |
The supplied information also identifies an XPI-S cold-end wire as an alternative for some applications. The final selection should be confirmed with the manufacturer because current capacity, ambient temperature, installation method, termination design, and certification requirements can affect compatibility.
Electrical heating systems require carefully selected protective devices. The product information recommends the use of a 30 mA leakage protection device for maximum safety and fire prevention. Where the design may result in higher leakage current, a device up to 300 mA may be necessary, subject to the applicable standards and project requirements.
Leakage current can be influenced by cable length, insulation condition, temperature, moisture, installation configuration, and the characteristics of the electrical supply. Long heating circuits may produce greater cumulative leakage than short circuits. The protection strategy should therefore be established during design rather than added after installation.
Each circuit should be protected against overcurrent and short circuit by a suitable protective device. The rating must consider the calculated operating current, startup conditions, ambient temperature, conductor capacity, and the requirements of the local electrical code.
Temperature control is equally important. The supplied information states that reliable design principles or temperature limiters must be used to determine temperature levels. A control thermostat may regulate the normal operating temperature, while an independent high-limit device can provide protection against sensor failure, loss of process fluid, excessive insulation, or abnormal operating conditions.
Earth continuity should be verified through the nickel-plated copper braid and all associated terminations. The braid must be properly connected at both the appropriate cable termination and the system protective earth. Continuity testing, insulation resistance testing, resistance measurement, and functional testing should be recorded as part of commissioning.
Heating cable should not overlap unless the design specifically permits it. The stated minimum spacing between heating lines is 20 millimeters. Maintaining spacing helps avoid concentrated heat and reduces the risk of local overheating. Cable should also be kept away from surfaces or materials that cannot tolerate the expected temperature.
Before installation, the cable should be inspected for visible damage, contamination, moisture ingress, crushed sections, or jacket defects. The reel should be handled carefully, and the cable should not be pulled across sharp edges or dragged through debris.
The minimum bending radius must be respected. At 70°C, the supplied data specifies a minimum bending radius of 25 times the heating-wire diameter when the heating-wire diameter is less than 6 millimeters. When the heating-wire diameter is greater than 6 millimeters, the specified minimum bending radius is six times the heating-wire diameter. The wording should be confirmed against the current technical drawing because cable diameter and heating-wire diameter may not be identical.
During routing, the cable should follow the surface without kinks or abrupt bends. Bends should be gradual, particularly near terminations, junctions, valves, and supports. The cable should be secured using compatible fixing materials that will not cut, puncture, chemically attack, or excessively compress the outer jacket.
For pipe applications, the cable may be positioned at the lower side of a horizontal pipe when freeze protection is the priority, or distributed around the pipe when uniform temperature maintenance is required. The final layout depends on heat-loss calculations and process requirements.
Thermal insulation should be installed after testing the heating cable. The insulation must be dry and properly sealed against water ingress. Wet insulation can greatly increase heat loss, reduce efficiency, and create unsafe electrical conditions. A warning label should identify heat-traced equipment and provide information for maintenance personnel.
After installation, resistance and insulation tests should be repeated. Measurements should be compared with the expected values and recorded for future maintenance. If the measured values differ substantially from the design figures, the circuit should not be energized until the cause has been investigated.
The manufacturer, Santo Thermal Control Technology Co., Ltd., is described as a high-tech enterprise located in Jiangsu Province, an important center for China’s electric heating belt industry. The company integrates research, design, production, manufacturing, and sales. Its product portfolio includes constant-power heating belts, self-regulating heating belts, silicone rubber heating products, glass-fiber heating belts, mineral-insulated cables, snow-melting cables, and related accessories.
This broad product experience is valuable because industrial heating solutions rarely consist of a cable alone. A complete system may require cold-end wires, termination kits, temperature sensors, controllers, junction boxes, fixing accessories, insulation interfaces, and protective devices. Experience across several heating technologies can help the manufacturer compare alternatives and recommend a construction suited to the application.
The company reports more than 35 years of industry experience, an annual output exceeding 10,000 units, more than 2,000 distributors, and business activity in more than 85 areas. These figures indicate an established manufacturing and distribution structure capable of supporting both standard products and project-specific requirements.
Product development has been a continuing focus. The company reports cooperation with Harvard University in the United States, the establishment of an irradiation center, development of high-temperature self-limiting heating technology, invention of carbon-fiber parallel heating cable technology, and construction of a product simulation testing laboratory. These activities support the development of heating systems intended for different temperature, environmental, and control conditions.
The manufacturing process for a polymer-insulated resistive cable requires close control of several stages. The conductor must have consistent resistance and reliable nickel plating. Stranding must maintain the specified geometry without creating sharp projections. Insulation extrusion must produce a continuous, concentric, void-free layer. The protective braid must provide sufficient coverage and mechanical stability. The final PTFE jacket must be uniform and free from defects that could compromise chemical resistance or electrical insulation.
Production inspection may include dimensional checks, resistance measurement, temperature coefficient verification, insulation testing, earth-braid continuity testing, visual inspection, and sampling of mechanical properties. For project applications, additional tests may be required according to the relevant standards, certification documents, and customer specifications.
The company states that it has passed ISO 9001 quality management system certification and that its products have obtained national CCC certification. It also reports explosion-proof certification and EAC Eurasian Union certification for relevant products. Certification status can vary by product model and production version, so buyers should request the current certificate that specifically applies to the XPI cable and the intended market.
The supplied product information states that supply length depends on the resistance model and is limited by a maximum reel weight of 120 kilograms, with each section being 1,000 meters. Not all models are standard stock items, and availability may vary. Buyers should confirm production lead time, reel length, packaging, labeling, and shipping conditions before placing an order.
For large industrial projects, purchasing should be based on a cable schedule that includes model number, resistance, required length, supply voltage, design power, installation zone, cold-end type, termination accessories, and control equipment. This reduces the risk of receiving a technically correct cable that does not match the project’s circuit design.
Customization may be possible for resistance, length, cold-end arrangement, packaging, labeling, and accessories, subject to engineering review. A custom product should not be ordered only by specifying watts per meter. The manufacturer should also receive information about pipe or equipment dimensions, operating temperature, ambient conditions, chemical exposure, hazardous-area classification, insulation, voltage, circuit length, and control method.
The primary reason to select the XPI series is its combination of temperature resistance, chemical protection, mechanical reinforcement, and electrical design flexibility. Many heating applications involve more than one challenge. A product may need to tolerate high temperature while also resisting solvents, withstand installation handling, operate outdoors, and maintain electrical integrity over long service periods.
The layered construction directly addresses these requirements. Nickel plating protects the conductor in demanding environments. Fluoropolymer insulation provides high-temperature electrical isolation. The nickel-plated copper braid improves mechanical protection and grounding. The PTFE jacket creates a chemically resistant outer barrier.
The broad resistance range is another important benefit. Engineers can select lower or higher resistance models according to the required power distribution and circuit length. This is more adaptable than a narrow product range in which the same cable must be forced into many different applications.
The product is also supported by a manufacturer with experience across several electric heating technologies. This can be advantageous for customers requiring a complete solution rather than a simple cable purchase. System design, control, cold-end selection, hazardous-area considerations, and commissioning guidance can be coordinated more efficiently when the supplier understands the full heating system.
Before selecting the XPI cable, determine the required maintained temperature and the minimum design ambient temperature. Calculate the heat loss through the pipe or equipment surface, including wind, insulation, supports, valves, flanges, and fittings.
Select the cable model according to resistance, voltage, circuit length, power output, and allowable current. Account for resistance variation with temperature and verify the actual operating current at the expected conductor temperature.
Confirm the maximum exposure temperature and the required continuous or intermittent duty. Verify that the cable, cold end, termination, sensors, control devices, and insulation can all tolerate the intended temperature.
Identify whether the installation is located in an ordinary, wet, corrosive, gas-hazardous, or dust-hazardous area. Confirm the certification and temperature classification of the complete system.
Specify the minimum bending radius, heating-line spacing, fixing method, thermal insulation, moisture sealing, grounding method, and test procedure.
Select circuit breakers, residual-current protection, temperature controllers, independent limiters, contactors, junction boxes, glands, and other accessories according to the calculated load and applicable standards.
Prepare installation drawings and cable schedules. Record resistance and insulation test results before and after installation. Provide operating and maintenance instructions for the end user.
The XPI series is a polymer-insulated resistive heating cable classified as a series constant-power heating cable. It is used for industrial heat tracing, temperature maintenance, freeze protection, and process heating.
The cable uses a nickel-plated stranded conductor, high-temperature fluoropolymer insulation, a nickel-plated copper braid, and a final PTFE outer jacket.
The supplied technical information specifies a maximum continuous exposure temperature of 260°C. It also specifies intermittent exposure up to 300°C for a maximum of 1,000 hours, subject to the applicable design conditions.
The fluoropolymer insulation and PTFE jacket are intended to provide resistance to organic and corrosive substances. Chemical compatibility must still be checked against the exact process chemicals, concentration, temperature, and exposure duration.
The supplied application information references gas Zones 1 and 2 and dust Zones 21 and 22. Suitability depends on the complete certified heating system, including cable, terminations, controls, grounding, installation method, and temperature limitation.
The listed standard maximum power output is 30 watts per meter. The actual permitted output depends on the application, installation surface, temperature control, spacing, insulation, and applicable certification requirements.
The nickel-plated copper braid provides additional mechanical protection and acts as a low-ohmic protective earth path when correctly terminated and connected to the grounding system.
The listed range extends from XPI-0.8 to XPI-8000, with standard resistance values from 0.8 ohm per kilometer to 8,000 ohms per kilometer at 20°C.
The correct resistance depends on supply voltage, heating length, required power, current capacity, heat loss, and operating temperature. It should be selected through a complete electrical and thermal design rather than by model number alone.
The supplied information recommends a 30 mA leakage protection device for maximum safety and fire prevention. Some high-leakage designs may require protection up to 300 mA, subject to local regulations and engineering verification.
The minimum installation temperature is listed as -70°C. Installation teams should nevertheless follow the current handling and bending instructions because cold conditions can affect flexibility and termination procedures.
The supplied technical data specifies a minimum spacing of 20 millimeters between heating lines. This spacing helps reduce concentrated heat and supports a more uniform temperature distribution.
Supply length depends on the resistance model and reel weight. Custom lengths and project-specific arrangements may be possible, but availability, minimum order quantities, packaging, and lead times should be confirmed before ordering.
The XPI cable is supplied by Santo Thermal Control Technology Co., Ltd., a Jiangsu-based manufacturer of electric heating and heat-tracing products. The company reports more than 35 years of industry experience and a product portfolio covering several heating technologies.
The XPI Polymer Insulated Series Resistive Heating Cable is designed for industrial applications that demand more than basic electrical heating. Its nickel-plated conductor, high-temperature fluoropolymer insulation, nickel-plated copper braid, and PTFE outer jacket create a layered construction suited to elevated temperatures, chemical exposure, mechanical handling, and demanding installation environments.
Its wide range of resistance values gives engineers flexibility when designing long or short circuits, low- or high-power systems, and different supply arrangements. Its listed temperature capability extends to 260°C continuously and 300°C intermittently under specified conditions. The product information also supports applications involving corrosive substances, cold installation environments, and classified hazardous areas when the complete system is properly engineered and certified.
The cable’s performance depends on correct design, installation, control, grounding, temperature limitation, insulation, and protection. For this reason, product selection should be treated as part of a complete heat-tracing system rather than as an isolated cable purchase. With appropriate engineering and verification, the XPI series can provide a durable and adaptable solution for pipeline tracing, process equipment heating, freeze protection, tank heating, and other industrial temperature-control duties.
1. XPI Product Specification, manufacturer-supplied technical document.
2. XPI Constant Watt Technology, manufacturer-supplied product information.
3. XPI Heating Systems, manufacturer-supplied system documentation.
4. XPI Product Description, manufacturer-supplied product literature.
5. EN 50019 reference cited in the supplied technical data for impact-resistance requirements.
6. ISO 9001 quality management principles referenced in the manufacturer’s company information.
7. Manufacturer-provided technical data for XPI resistance models, cold-end wires, temperature coefficients, dimensions, and standard weights.
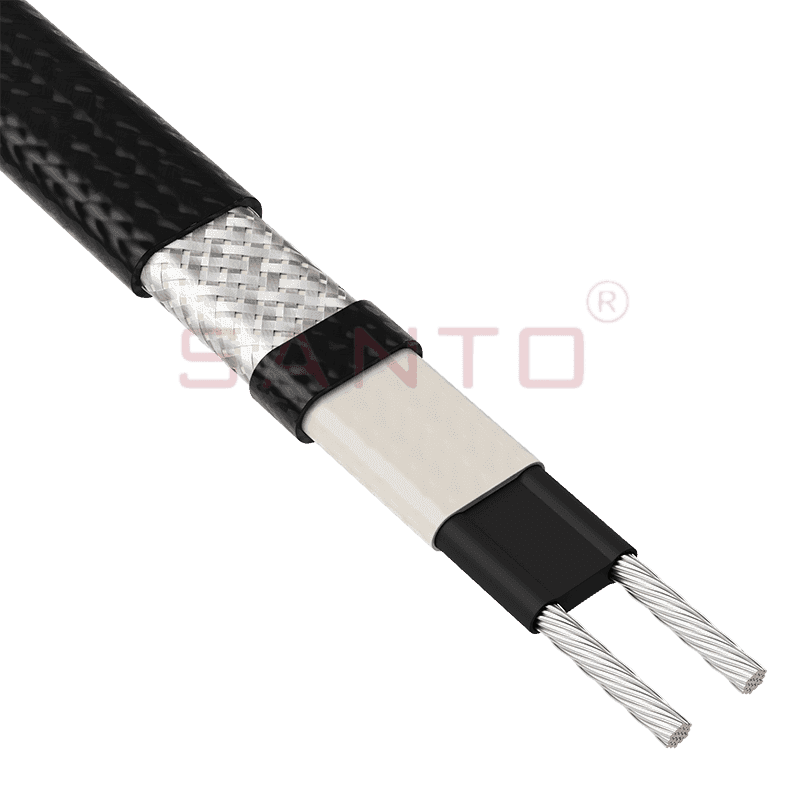
The SANTO UFA range of self-regulating heating cables is mainly used for frost protection of pipes and vessels but can also be used to maintain processes up to 65°C. These heating cables are available...
See Details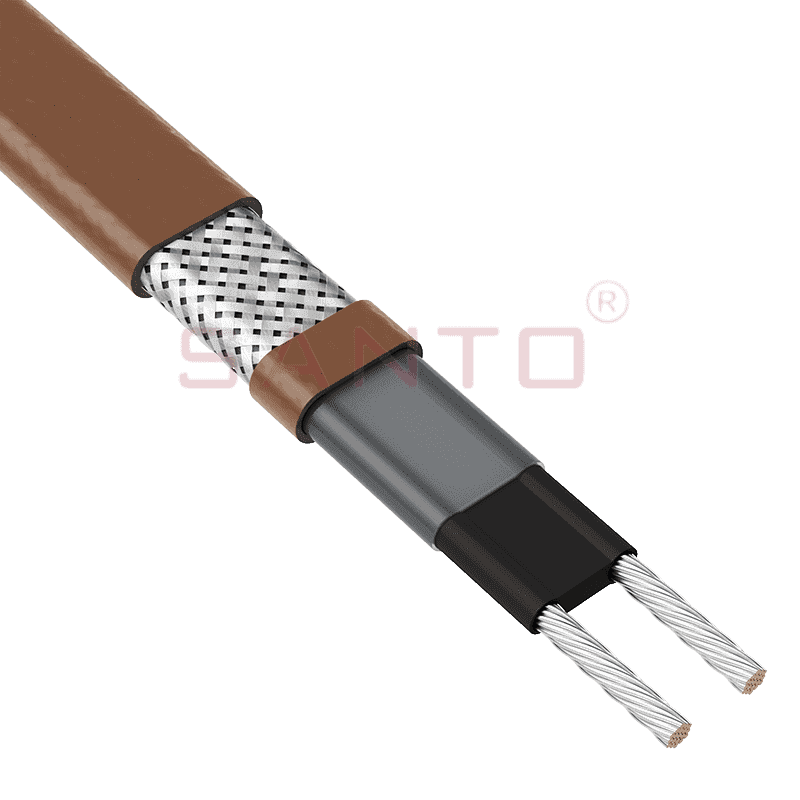
The SANTO UFB range of self-regulating heating cables is mainly used for frost protection of pipes and vessels requiring a higher power output than the UFA heating cables can supply. They can also be ...
See Details
The SANTO UFC range of self-regulating heating cables is used for frost protection of pipes and vessels that require steam cleaning. They can also be used to maintain processes up to 121°C. These heat...
See Details
The SANTO UFO range of self-regulating heating cables is mainly used for frost protection of pipes and vessels that require steam cleaning . They can also be used to maintain processes up to 150°C. Th...
See Details
The SANTO UFD series of self-regulating heating cables are mainly used for freeze protection of pipes and vessels, but can also be used to maintain processes up to 200°C. These heating cables are avai...
See Details
SANTO UFY heating wire is suitable for applications that maintain process temperatures up to 260 ℃ and can be steam blown; The self-regulating and parallel circuit heating wires of the UFY series are ...
See Details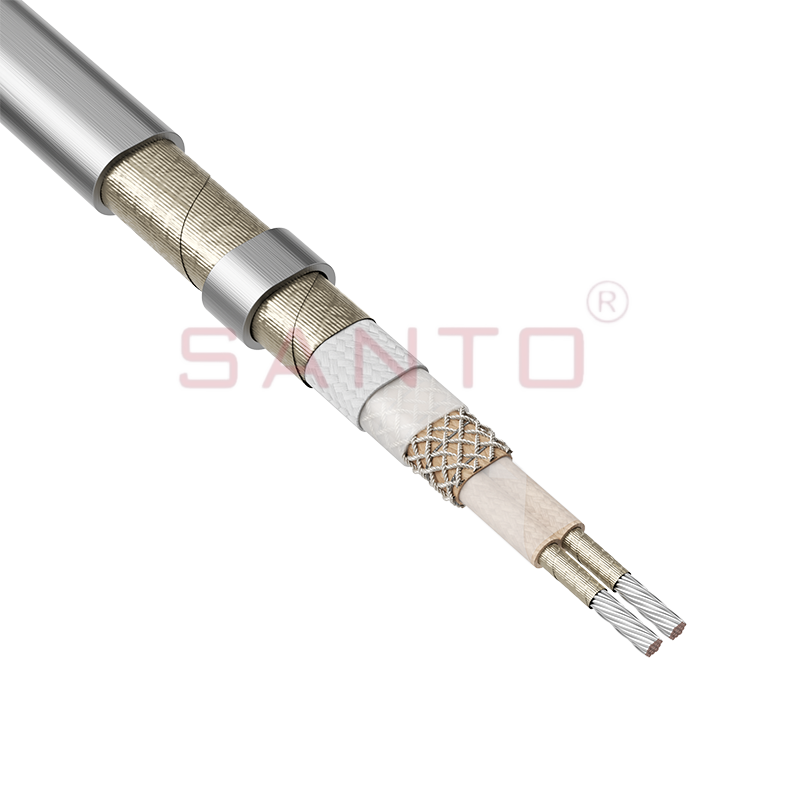
The SANTO UFM series self-regulating heating cables are mainly used for freeze protection of pipes and vessels, but can also be used to maintain processes up to 400°C. These heating cables are availab...
See Details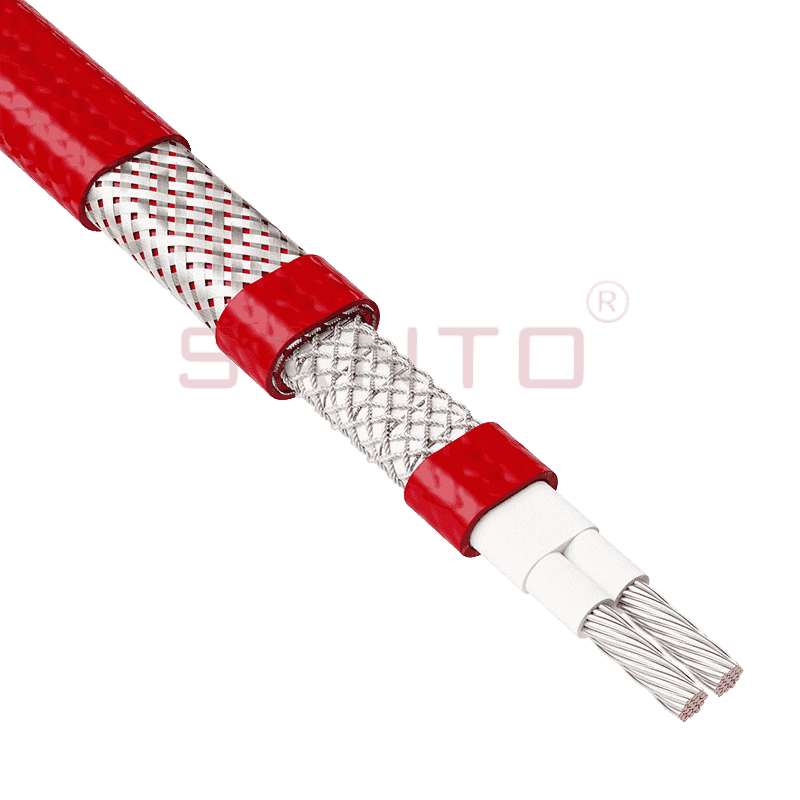
The SANTO ACC range of power-limiting heating cables is mainly used for temperature maintenance of processes and offers the advantage of a high power output at high temperatures which can reduce the n...
See Details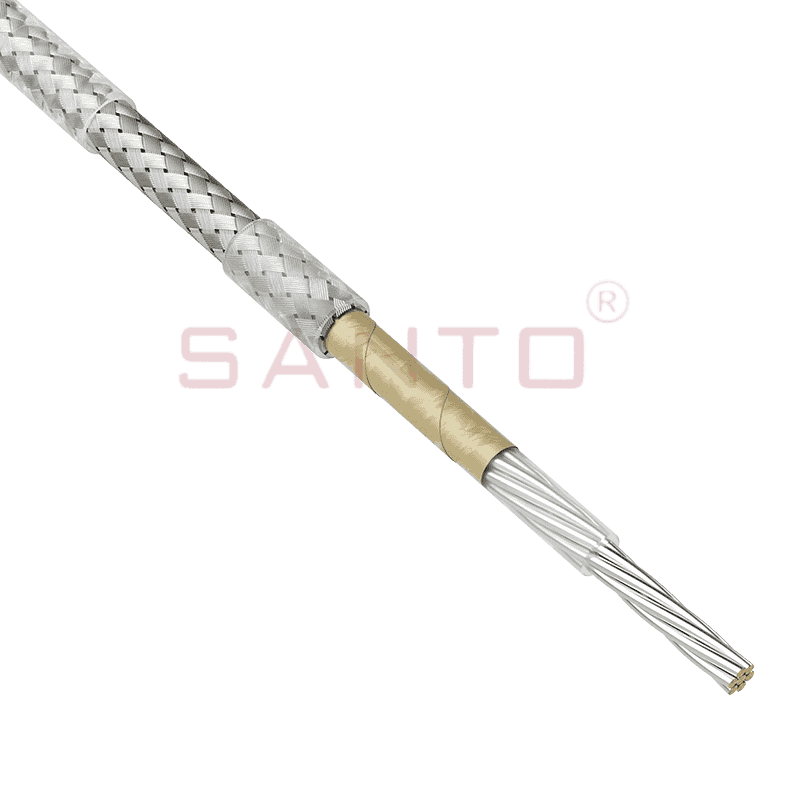
The stranded high temperature conductor is nickel plated to ensure a long life at elevated temperatures in corrosive environments. It is electrically isolated using an innovative sandwich construction...
See Details
The stranded high temperature conductor is nickel plated to ensure a long life at elevated temperatures in corrosive environments. It is electrically isolated using an innovative sandwich construction...
See Details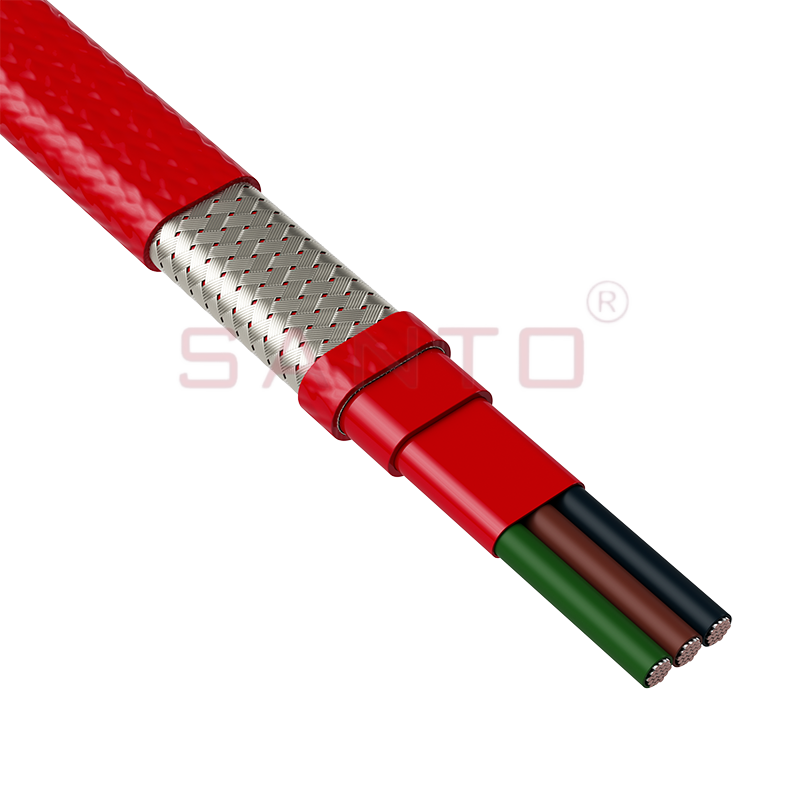
The stranded high temperature conductor is nickel plated to ensure a long life at elevated temperatures in corrosive environments. It is electrically isolated using an innovative sandwich construction...
See Details
SANTO HAx mineral insulated (MI) Alloy 825 series heating cables are suitable for use in hazardous areas. They have been designed for use in freeze protection and temperature maintenance applications ...
See Details
Santo electric heating strips are widely used in key industries in China.

